Call: 08071724944
 Send Inquiry

 Send Inquiry
Mono Ethylene Glycol
Price 85 INR/ Kilograms
MOQ : 50 Kilograms
Mono Ethylene Glycol Specification
- Properties
- Colorless, odorless, viscous
- Product Type
- Chemical
- Solubility
- Miscible with water
- CAS No
- 107-21-1
- Smell
- Odorless
- Ingredients
- Mono Ethylene Glycol
- Appearance
- Clear liquid
- Melting Point
- -12.9C
- HS Code
- 29053100
- EINECS No
- 203-473-3
- Poisonous
- YES
- Shelf Life
- 2 years
- Application
- Coolants, antifreeze, polyester
- Ph Level
- ~7 (neutral)
- Refractive Rate
- 1.4314
- Storage
- Store in tightly sealed container
- Usage
- Industrial chemical processes
- Molecular Weight
- 62.07 g/mol
- Density
- 1.115 Gram per cubic centimeter(g/cm3)
- Taste
- Sweetish
- Structural Formula
- HOCH2CH2OH
- Grade
- Technical
- Purity
- 99% min
- Physical Form
- Liquid
- Molecular Formula
- C2H6O2
- Transport
- Non-hazardous
- Form
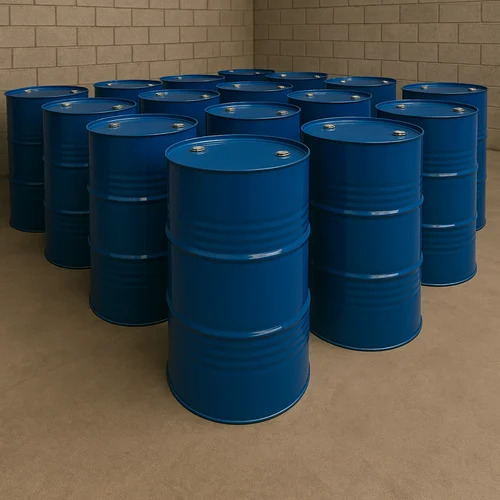
- Liquid barrels
- Grade Standard
- Industrial Grade
- Color
- Colorless
- Packaging Details
- 230 kg Drum
- Packaging Type
- HDPE barrel
Mono Ethylene Glycol Trade Information
- Minimum Order Quantity
- 50 Kilograms
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 5000 Kilograms Per Month
- Delivery Time
- 7 Days
- Main Domestic Market
- All India
About Mono Ethylene Glycol
Purchase Mono Ethylene Glycol (MEG), a highlighted industrial-grade chemical acknowledged for its valiant versatility and noteworthy purity of 99% minimum. Presented in non-hazardous HDPE barrels (230 kg drums), this colorless, odorless, and viscous liquid is in demand across cooling, antifreeze, and polyester production industries. Its astonishing characteristics-such as miscibility with water, sweetish taste, and neutral pH-make it essential for numerous technical applications. Notably, its structural integrity and long shelf life underscore MEG's superiority for suppliers and traders throughout India.
Industrial Usage and Plant Applications of Mono Ethylene Glycol
Mono Ethylene Glycol stands out as a noteworthy solution for diverse industrial processes. Its primary usage lies in coolants, antifreeze formulations, and polyester manufacturing, making it highly demanded by various plants and factories. Highlighted for its technical grade and valiant performance, it is well-suited as an essential intermediate in both large-scale and specialized operations. Its versatility and miscibility with water amplify its significance as an industrial chemical for multiple plant applications across sectors.
Delivery, Packaging, and Sample Exchange
Exchange and freight for Mono Ethylene Glycol are managed with efficiency, ensuring timely dispatching in robust HDPE barrels weighing 230 kg each. Packaging details guarantee safe transport and prolonged product integrity. Customers can request samples to evaluate quality prior to large-scale purchase, making the process transparent and reliable. With seamless delivery timelines and accessible sample exchange, clients experience a noteworthy value in logistics and satisfaction from order to receipt.
FAQ's of Mono Ethylene Glycol:
Q: How is Mono Ethylene Glycol commonly used in industrial applications?
A: Mono Ethylene Glycol is primarily used in manufacturing coolants, antifreeze, and polyester resins. It also finds application as an intermediate in various industrial chemical processes due to its miscibility and technical grade purity.Q: What packaging type and size is available for Mono Ethylene Glycol delivery?
A: Mono Ethylene Glycol is supplied in 230 kg HDPE barrels, designed to ensure safe, non-hazardous transport and convenient storage in industrial settings.Q: When can customers expect the delivery of Mono Ethylene Glycol after placing an order?
A: Delivery times are typically efficient, with dispatching arranged promptly after order confirmation, ensuring minimal delays in freight and product receipt.Q: Is a sample of Mono Ethylene Glycol available for evaluation before full purchase?
A: Yes, samples can be exchanged and provided upon request, allowing clients to assess the quality and appropriateness for their intended applications before committing to bulk orders.Q: What are the main benefits of using industrial-grade Mono Ethylene Glycol?
A: Industrial-grade Mono Ethylene Glycol boasts a purity of 99%, excellent water solubility, and a neutral pH. These features ensure noteworthy performance in coolants, antifreeze, and industrial chemical processes, providing reliability across applications.Q: Where should Mono Ethylene Glycol barrels be stored to ensure product integrity?
A: It is recommended to store Mono Ethylene Glycol barrels in a tightly sealed container in a dry, well-ventilated area, away from direct sunlight and incompatible chemicals, to maintain their shelf life and quality.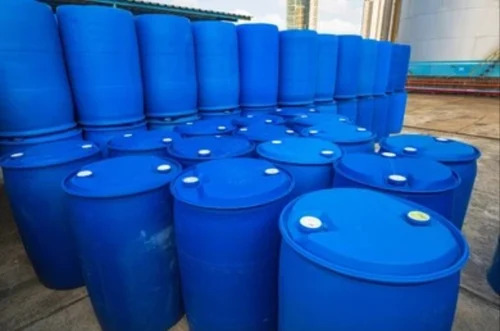
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Industrial Chemicals Category
Xanthan Gum Powder
Price 285 INR / Kilograms
Minimum Order Quantity : 50 Kilograms
Product Type : Hydrocolloid / Food Additive
Purity : >98%
Physical Form : Powder
Appearance : Offwhite to cream powder
Chlorhexidine Gluconate Solution
Price 290 INR / Kilograms
Minimum Order Quantity : 50 Kilograms
Product Type : Chemical Solution
Purity : 20% w/v
Physical Form : Liquid
Appearance : Clear, colorless to pale yellow liquid
Zinc Pyrithione Powder
Price 785 INR / Kilograms
Minimum Order Quantity : 50 Kilograms
Product Type : Raw Material
Purity : 99%
Physical Form : Powder
Appearance : White fine powder
Tolune Chemical Solvent
Price 98 INR / Kilograms
Minimum Order Quantity : 50 Kilograms
Product Type : Chemical Solvent
Purity : 99%
Physical Form : Liquid
Appearance : Clear, colorless liquid

Contact Details
Insta Chemi Private Limited
GST : 09AAGCI0124E1Z1
- H-174, SECTOR 63, Noida - 201301, Uttar Pradesh, India
- Phone :08071724944
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
